.gtr-container-a7f3k {
font-family: Verdana, Helvetica, "Times New Roman", Arial, sans-serif;
font-size: 14px;
line-height: 1.6;
color: #1a1a2e;
max-width: 100%;
box-sizing: border-box;
padding: 8px 0;
}
.gtr-container-a7f3k *,
.gtr-container-a7f3k *::before,
.gtr-container-a7f3k *::after {
box-sizing: border-box;
}
.gtr-container-a7f3k .gtr-h2-a7f3k {
font-size: 18px;
font-weight: bold;
color: #0000FF;
margin: 28px 0 12px 0;
padding: 0 0 8px 0;
border-bottom: 2px solid #ccd0ff;
line-height: 1.4;
letter-spacing: 0.2px;
}
.gtr-container-a7f3k .gtr-h2-a7f3k:first-child {
margin-top: 0;
}
.gtr-container-a7f3k p {
font-size: 14px;
line-height: 1.6;
text-align: left;
margin: 0 0 14px 0;
color: #2b2b3a;
}
.gtr-container-a7f3k strong {
color: #0000CC;
font-weight: bold;
}
.gtr-container-a7f3k ul,
.gtr-container-a7f3k ol {
list-style: none !important;
margin: 0 0 16px 0;
padding: 0;
}
.gtr-container-a7f3k ul li,
.gtr-container-a7f3k ol li {
position: relative;
padding: 6px 0 6px 24px;
font-size: 14px;
line-height: 1.6;
text-align: left;
color: #2b2b3a;
border-bottom: 1px solid #eef0ff;
}
.gtr-container-a7f3k ul li:last-child,
.gtr-container-a7f3k ol li:last-child {
border-bottom: none;
}
.gtr-container-a7f3k ul li::before {
content: "•" !important;
position: absolute !important;
left: 0 !important;
top: 6px;
color: #0000FF;
font-weight: bold;
font-size: 14px;
line-height: 1.6;
}
.gtr-container-a7f3k ol {
counter-reset: list-item;
}
.gtr-container-a7f3k ol li::before {
content: counter(list-item) "." !important;
position: absolute !important;
left: 0 !important;
top: 6px;
color: #0000FF;
font-weight: bold;
font-size: 14px;
line-height: 1.6;
}
.gtr-container-a7f3k .gtr-table-wrap-a7f3k {
width: 100%;
overflow-x: auto;
margin: 0 0 18px 0;
border-radius: 8px;
box-shadow: 0 2px 10px rgba(0, 0, 255, 0.08);
}
.gtr-container-a7f3k table {
width: 100%;
border-collapse: collapse !important;
border-spacing: 0 !important;
border: 1px solid #b8bfff !important;
font-size: 14px;
background: #ffffff;
min-width: 520px;
}
.gtr-container-a7f3k table th {
background: #0000FF !important;
color: #ffffff !important;
font-weight: bold !important;
font-size: 14px !important;
text-align: left !important;
padding: 10px 12px !important;
border: 1px solid #0000CC !important;
line-height: 1.5 !important;
word-break: normal !important;
overflow-wrap: break-word !important;
}
.gtr-container-a7f3k table td {
padding: 9px 12px !important;
border: 1px solid #ccd0ff !important;
color: #2b2b3a !important;
font-size: 14px !important;
text-align: left !important;
line-height: 1.5 !important;
vertical-align: top !important;
word-break: normal !important;
overflow-wrap: break-word !important;
background: #ffffff !important;
}
.gtr-container-a7f3k table tbody tr:nth-child(even) td {
background: #f4f5ff !important;
}
.gtr-container-a7f3k table tbody tr:hover td {
background: #e8eaff !important;
}
@media (min-width: 768px) {
.gtr-container-a7f3k {
padding: 12px 4px;
}
.gtr-container-a7f3k .gtr-h2-a7f3k {
font-size: 18px;
margin: 34px 0 14px 0;
}
.gtr-container-a7f3k p {
margin: 0 0 16px 0;
}
.gtr-container-a7f3k table {
min-width: 0;
}
}
Project Overview
A filament producer in Malaysia ordered a PLA ABS PETG TPU 3D printer filament extruder machine from Friend Plastic Machine — the CE certified FLD-45 single screw line — to replace toll-produced filament with in-house production. The brief was unusual in one respect: the client wanted one machine, four polymers. PLA, ABS, PETG and TPU all had to run on the same 45 mm extruder with no screw change, only a die and temperature recipe change. The line was built, trial-run on the customer's own resins in our Zhangjiagang workshop, shipped in 30 working days, and has been running three polymer families commercially since commissioning, with TPU added in the third month.
Customer Background
The buyer supplies 1.75 mm filament to Malaysian 3D printing service bureaus, school STEM programmes and a growing base of industrial users in Johor and Selangor. Sourcing finished filament from third-party extruders gave them 4–6 week lead times, no control over batch-to-batch diameter, and no short colour campaigns for local resellers. Their target was an in-house line that could switch between commodity materials in a single shift.
Malaysia's year-round humidity is unforgiving to hygroscopic polymers, so moisture control rather than line speed became the decisive issue.
Materials and Process Requirements
MaterialBarrel TemperaturePre-dryingPractical Output
PLA190–210 °C45 °C / 4 h20–22 kg/h
ABS230–250 °C75 °C / 4 h19–21 kg/h
PETG235–250 °C65 °C / 5 h18–20 kg/h
TPU (95A)195–215 °C80 °C / 4 h12–15 kg/h
All four materials had to hold 1.75 mm ±0.03 mm, because the client's service-bureau customers print on both Bowden and direct-drive machines where diameter drift shows up immediately as under-extrusion or jams. TPU set the hardest constraint: soft pellets feed unevenly, generate more die swell, and need gentler screw compression and tighter haul-off control than rigid polymers.
Machine Configuration Supplied
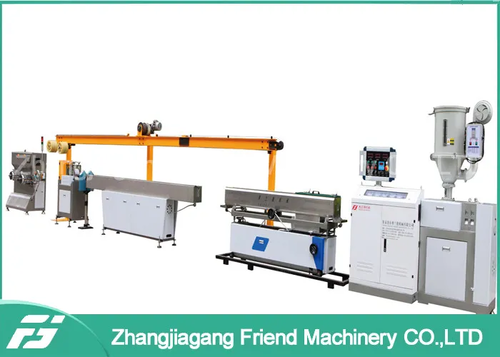
FLD-45 / SJ-45 single screw extruder, 45 mm screw, 15 kW drive, general-purpose screw geometry suitable for both rigid and soft polymers
1.75 mm strand die and calibration plate set, plus a 3.0 mm set for industrial users
Two 3 m water cooling baths with calibration — extended cooling is what keeps TPU round rather than oval
Caterpillar haul-off unit with fine speed control for soft filament
Variable speed wind-up station for 1–5 kg spools
Hopper dryer with dehumidified air, sized for the Malaysian climate
CE certified electrical cabinet, guarded rotating parts, emergency stop circuit
Commissioning and Material Trials
A Friend commissioning engineer spent eight days on site in Malaysia. The first three days were mechanical: levelling the 17 m line, setting die and calibration gaps, and establishing stable haul-off tension. The remaining days were dedicated to material trials, working through the four polymers in sequence so the client's operators could see how the same line responds differently to each one:
Temperature profile and screw speed settings for PLA, ABS, PETG and TPU
Drying routine for each polymer, including a check that showed visibly bubbling PETG before drying and clean filament after
Die swell compensation and calibration plate adjustment for TPU
Purge procedure when switching from ABS to PLA to avoid black specks in light colours
Diameter measurement and tolerance logs per spool
Results Achieved
MetricRequirementResult
Materials on one linePLA, ABS, PETG, TPUAll four running commercially
Output on PLA20 kg/h20–22 kg/h
Output on TPUUsable commercial rate12–15 kg/h, stable
Diameter tolerance1.75 mm ±0.03 mm±0.02–0.03 mm on all four polymers
Material changeoverSame shiftUnder 60 minutes including purge
Batch consistencyReduce customer complaintsNo diameter-related rejections in first six months
Within six months the client had moved roughly 70 % of their filament volume in house, run two short colour campaigns without an outside extruder, and added a TPU line they had never been able to source reliably.
Why This Client Chose Friend Plastic Machine
Four polymers on one extruder — no second machine for TPU
CE certified build with documentation accepted at Malaysian customs
Trial run before shipment on the customer's own resins, video approved remotely
30 working day lead time and PE film plus wood case packing for sea freight
On-site commissioning in English, plus spare dies and calibration plates held in stock
Conclusion
A multi-material filament line only works if the screw, cooling length, haul-off and drying stage are sized for the most difficult polymer in the recipe — in this case TPU — not for PLA alone. If you are evaluating a PLA, ABS, PETG or TPU 3D printer filament extruder machine for your own market, send us your material list, target diameter and available floor length, and our engineers will propose a configuration and a material trial plan built around your resins.
.gtr-container-k7m2{font-family:Verdana,Helvetica,"Times New Roman",Arial,sans-serif;font-size:14px;line-height:1.6;color:#1a1a2e;text-align:left;max-width:100%;box-sizing:border-box;padding:4px;}
.gtr-container-k7m2 *,.gtr-container-k7m2 *::before,.gtr-container-k7m2 *::after{box-sizing:border-box;}
.gtr-container-k7m2 .gtr-h2{font-size:18px;font-weight:bold;color:#0000FF;margin:28px 0 12px;padding-bottom:8px;border-bottom:2px solid #d6d6ff;line-height:1.4;}
.gtr-container-k7m2 .gtr-h2:first-child{margin-top:0;}
.gtr-container-k7m2 p{margin:0 0 14px;text-align:left;line-height:1.6;font-size:14px;color:#1a1a2e;}
.gtr-container-k7m2 strong{color:#0000CC;font-weight:bold;}
.gtr-container-k7m2 ul,.gtr-container-k7m2 ol{list-style:none !important;margin:0 0 16px;padding:0;}
.gtr-container-k7m2 ul li,.gtr-container-k7m2 ol li{position:relative;padding-left:22px;margin:0 0 9px;line-height:1.6;font-size:14px;color:#1a1a2e;}
.gtr-container-k7m2 ul li::before{content:"•" !important;position:absolute !important;left:0 !important;top:0;color:#0000FF;font-weight:bold;}
.gtr-container-k7m2 ol li::before{content:counter(list-item) "." !important;position:absolute !important;left:0 !important;top:0;color:#0000FF;font-weight:bold;}
.gtr-container-k7m2 .gtr-table-wrap{overflow-x:auto;margin:0 0 18px;border-radius:8px;box-shadow:0 2px 10px rgba(0,0,255,0.08);}
.gtr-container-k7m2 table{width:100%;border-collapse:collapse !important;border-spacing:0 !important;font-size:14px;border:1px solid #c3c3f0 !important;background:#ffffff;}
.gtr-container-k7m2 table th,.gtr-container-k7m2 table td{border:1px solid #c3c3f0 !important;padding:10px 12px !important;text-align:left !important;vertical-align:top;line-height:1.5;word-break:normal;overflow-wrap:break-word;}
.gtr-container-k7m2 table th{background:#0000FF !important;color:#ffffff !important;font-weight:bold;white-space:nowrap;}
.gtr-container-k7m2 table tbody tr:nth-child(even) td{background:#f4f4ff !important;}
.gtr-container-k7m2 table tbody tr:hover td{background:#e6e6ff !important;}
@media (min-width:768px){
.gtr-container-k7m2{padding:8px 12px;}
.gtr-container-k7m2 .gtr-h2{font-size:18px;margin:32px 0 14px;}
.gtr-container-k7m2 table th,.gtr-container-k7m2 table td{padding:12px 16px !important;}
}
Project Overview
In 2026 a 3D printing filament manufacturer based in Southeast Asia placed an order with Friend Plastic Machine (Zhangjiagang Friend Machinery Co., Ltd.) for a 20kg capacity 3D printer filament machine — the FLD-45 single screw PLA filament extruder machine with CE certification. The line was specified for continuous production of 1.75 mm PLA filament feeding the client's own 3D printing consumable brand, with a secondary capability to run ABS, PETG and PA simply by changing the strand die and calibration plates. From deposit to container loading the project was completed in 30 working days, and the line has been running two shifts a day since commissioning at a stable 20–22 kg/h output.
Customer Background
The buyer is a filament and 3D printing consumables supplier serving Southeast Asia's fast-growing desktop 3D printer aftermarket. Their existing single small extruder (around 8 kg/h) could no longer cover demand from local resellers, and outsourced filament was eroding both margin and colour consistency. Their purchasing team set three non-negotiable conditions for the upgrade:
Real output above 20 kg/h on PLA, not a laboratory figure
Diameter tolerance tight enough for modern direct-drive printers (1.75 mm ±0.03 mm)
CE certification accepted by their customs and by their own downstream customers
Technical Requirements
ParameterClient RequirementFriend FLD-45 Solution
Capacity20 kg/h minimumSJ-45 single screw extruder, 20–22 kg/h on PLA
Screw diameterIndustrial single screw45 mm, dedicated PLA/PETG screw geometry
Filament diameter1.75 mm ±0.03 mm1.75 mm die set, optional 2.85 mm / 3.0 mm sets
CoolingConsistent ovality controlTwo 3 m water cooling baths with calibration plates
Haul-off & windingAutomatic tension controlCaterpillar haul-off + variable speed wind-up station
ComplianceCE for import clearanceCE certified machine, CE-compliant control cabinet
Lead timeUnder 45 days30 working days, PE film + wood case packing
Machine Configuration Supplied
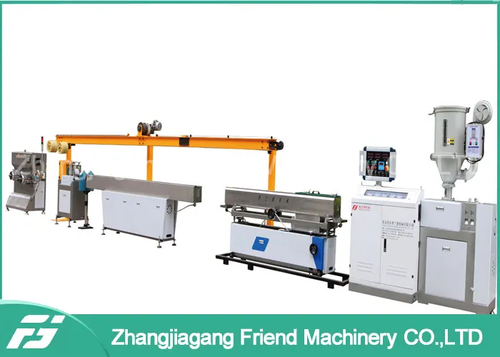
FLD-45 / SJ-45 single screw extruder — frequency-controlled drive, water cooling, raw material PLA / ABS / PA
1.75 mm strand die and calibration plate set, with spare 2.85 mm and 3.0 mm sets quoted for future SKUs
Two 3 m water cooling baths with calibration — the second bath stabilises diameter after the first cooling stage
Caterpillar haul-off unit for slip-free pulling and stable line speed
Variable speed wind-up station for even spool tension up to 5 kg bobbins
CE electrical cabinet with emergency stop circuit and guarded rotating parts
Commissioning and Operator Training
Before shipment the complete line was assembled and trial-run in our Zhangjiagang workshop on the client's own PLA pellets, and a video of the run was sent for approval. After the container arrived, a Friend commissioning engineer attended site for seven days to level the 17 m line, set the die and calibration gap, tune bath temperature and haul-off speed, and train four operators. The client's team was walked through:
Start-up, shutdown and emergency procedures
Screw and barrel temperature profiles for PLA, ABS and PETG
Diameter adjustment through calibration plate and haul-off speed
Daily cleaning of the die, filter and cooling baths
Fault diagnosis for diameter drift, ovality and moisture-related bubbles
Remote support continues over video call and chat, with spare dies and calibration plates held in stock for fast dispatch.
Measured Results on Site
MetricTargetMeasured After Commissioning
Output on PLA20 kg/h20–22 kg/h continuous
Diameter tolerance±0.03 mm±0.02–0.03 mm over 1.75 mm
Start-up scrapBelow 5 %Under 2 % after operator training
Line footprintFit existing hall17 m total length, single operator
Shifts runningTwo shiftsTwo shifts daily, no unplanned stoppage in first 90 days
With the new line the client brought filament production back in house, doubled usable capacity versus their 8 kg/h machine, and gained the colour consistency their resellers asked for. The CE certificate also cleared import formalities without a single technical query.
Why the Client Chose Friend Plastic Machine
Verified capacity, not catalogue claims — trial run on the customer's own PLA before shipment
CE certification on the machine itself, accepted by customs and downstream buyers
Extruder platform flexibility — one machine covers PLA, ABS, PETG and PA with die changes
30 working day lead time and sea-worthy PE film plus wood case packing
On-site commissioning and operator training in English, plus long-term spare parts support
Conclusion
This Southeast Asian project shows what a 20 kg/h capacity 3D printer filament machine can deliver when extruder, cooling, haul-off and winding stages are engineered as one line. If you are planning a PLA filament extruder investment — a single 20 kg/h line or a multi-line filament plant — our engineers can size the screw, die and cooling length around your resin, target diameter and certification needs. Send us your filament specification for a line layout and trial-run plan.
Heavy-Duty Plastic Extruder Machine for Industrial Sheet Production
Client BackgroundA large-scale plastic sheet manufacturer in Spain supplies ABS and PP sheets for automotive and appliance industries.
Production Challenges
High material output requirements
Continuous heavy-duty operation
Strict surface quality standards
Engineering SolutionA high-torque Plastic Extruder Machine with reinforced gearbox and optimized screw geometry for thick sheet extrusion.
Measured ResultsThe machine maintained stable pressure and temperature control during 24/7 operation. Sheet flatness and surface quality met high-end industrial standards.
Customer Statement
“The durability and output stability of this Plastic Extruder Machine are impressive. It performs reliably even under intensive production schedules.”
ConclusionThis successful project strengthened long-term cooperation and positioned the extruder as a core production asset.
Plastic Extruder Machine for Profile Extrusion in Italy
Project OverviewAn Italian manufacturer produces plastic window and door profiles for residential construction.
Technical Requirements
High dimensional accuracy
Smooth surface finish
Flexible mold compatibility
Delivered SolutionWe supplied a precision Plastic Extruder Machine integrated with a customized calibration table and cooling system.
Operational ResultsThe extrusion line delivered precise profiles with minimal post-processing. Production efficiency improved, and defect rates dropped significantly.
Customer Testimonial
“This Plastic Extruder Machine provides excellent control and repeatability. It fits perfectly into our existing production workflow.”
Future PlansThe customer plans to expand capacity using the same extruder model for additional profile designs.
Plastic Extruder Machine for Recycling Applications in Eastern Europe
Application ScenarioA recycling company in Poland focuses on converting post-consumer plastic waste into reusable granules.
Project ObjectiveTo process mixed plastic materials efficiently while maintaining stable extrusion output.
Recommended EquipmentA twin-screw Plastic Extruder Machine with degassing system and reinforced screw elements designed for recycled plastics.
Performance Highlights
Strong material mixing capability
Effective removal of moisture and impurities
Stable pellet quality
Customer Evaluation
“The Plastic Extruder Machine handles recycled materials much better than our previous system. Output quality is very consistent.”
Long-Term CooperationAfter six months of operation, the customer confirmed low maintenance requirements and placed follow-up orders for spare parts and upgrades.
Plastic Extruder Machine for PE Film Production in the United States
Client ProfileA packaging manufacturer in Texas produces PE stretch film and industrial packaging materials for logistics companies.
Key Challenges
Frequent downtime with old machines
Uneven film thickness
High maintenance costs
Customized ConfigurationWe delivered a high-speed Plastic Extruder Machine optimized for PE film extrusion, equipped with a high-performance screw design and automatic thickness control system.
Operational PerformanceThe machine achieved uniform melt flow and stable extrusion even during long production shifts. Film transparency and tensile strength were significantly improved.
Client Feedback
“This Plastic Extruder Machine has dramatically improved our product consistency and reduced production waste.”
Business ValueThe client reported a noticeable reduction in scrap rate and faster return on investment due to increased productivity.
Plastic Extruder Machine for PVC Pipe Manufacturing in Germany
Industry BackgroundA medium-sized plastic processing company in southern Germany specializes in PVC water supply and drainage pipes for municipal infrastructure projects. Due to increasing order volume, the client needed to upgrade their production line with a more efficient Plastic Extruder Machine.
Customer Needs
Stable long-term operation
High extrusion accuracy
Energy-efficient performance
Compliance with EU manufacturing standards
Solution ProvidedWe supplied a high-output single-screw Plastic Extruder Machine designed specifically for PVC pipe extrusion. The machine featured a precision screw and barrel system, advanced temperature control zones, and a Siemens-based control system for stable output.
Production ResultsAfter commissioning, the extrusion line achieved consistent wall thickness and smooth pipe surfaces. The output capacity increased by over 20%, while energy consumption per unit was reduced.
Customer Recognition
“The Plastic Extruder Machine runs extremely smoothly. Its extrusion stability and automation level fully meet German manufacturing standards.”
Project OutcomeThe client expanded cooperation by ordering an additional extruder line within the same year, confirming high satisfaction with both equipment quality and technical support.
The Christmas is coming.On this festival,we,Zhangjiagang Friend Machinery Co.,lTD,send most sincere congratulations to every customers and friends.Our staff also prepare a short video to convey our best wishes to everyone,hoping to bring good luck to everyone's Christmas and new year holiday.
Review 2021,the employees of sales department have made gratifying achievements,and the sales perfomance has also reached a higher level.The same is true of the workers in the technology department, who have made new breakthroughs in the production of many plastic machinery industries.We not only keep working hard through the whole year,we are also committed to improving our service quality and strive to provide best service to every customer.
In the new year 2022,welcome everyone to continue to choose and believe in us,Zhangjiagang Friend Machinery Co.,lTD.Wish everyone better future.
We value the trust and partnership we have with our clients. To strengthen these relationships, we are excited to introduce the opportunity for customer visits. We invite our clients to witness our operations firsthand, providing them with an immersive experience and a deeper understanding of our capabilities.
During the visit, clients will have the chance to:
Tour our Factory: Explore our state-of-the-art warehouses, loading areas, and equipment. Witness the meticulous planning and organization that goes into every shipment.
Meet Our Experts: Interact with our experienced team members who will be on hand to explain our processes, answer questions, and offer insights into industry best practices.
Gain Transparency: Understand the journey of your goods, from arrival at our facility to container loading and shipment. Witness our commitment to quality control and adherence to international standards.